Central China meat plant A: ammonia HP recovers refrigeration heat for plant hot water
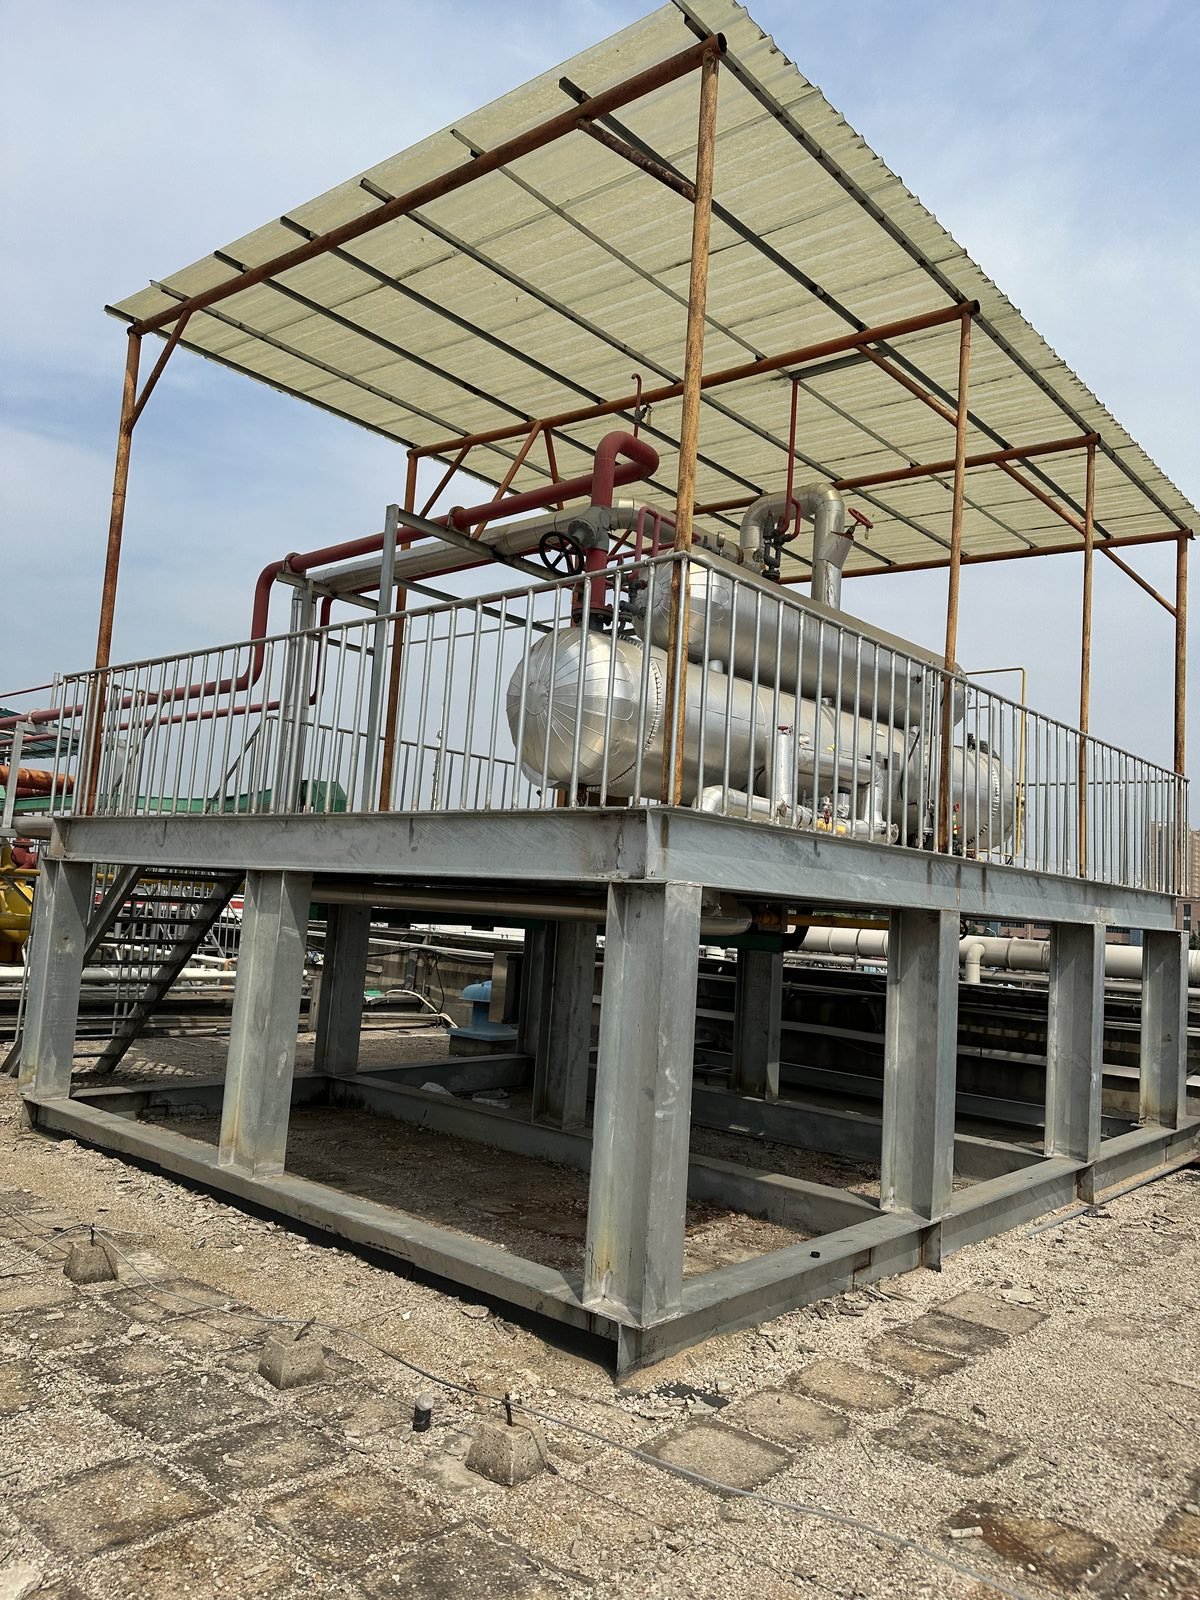
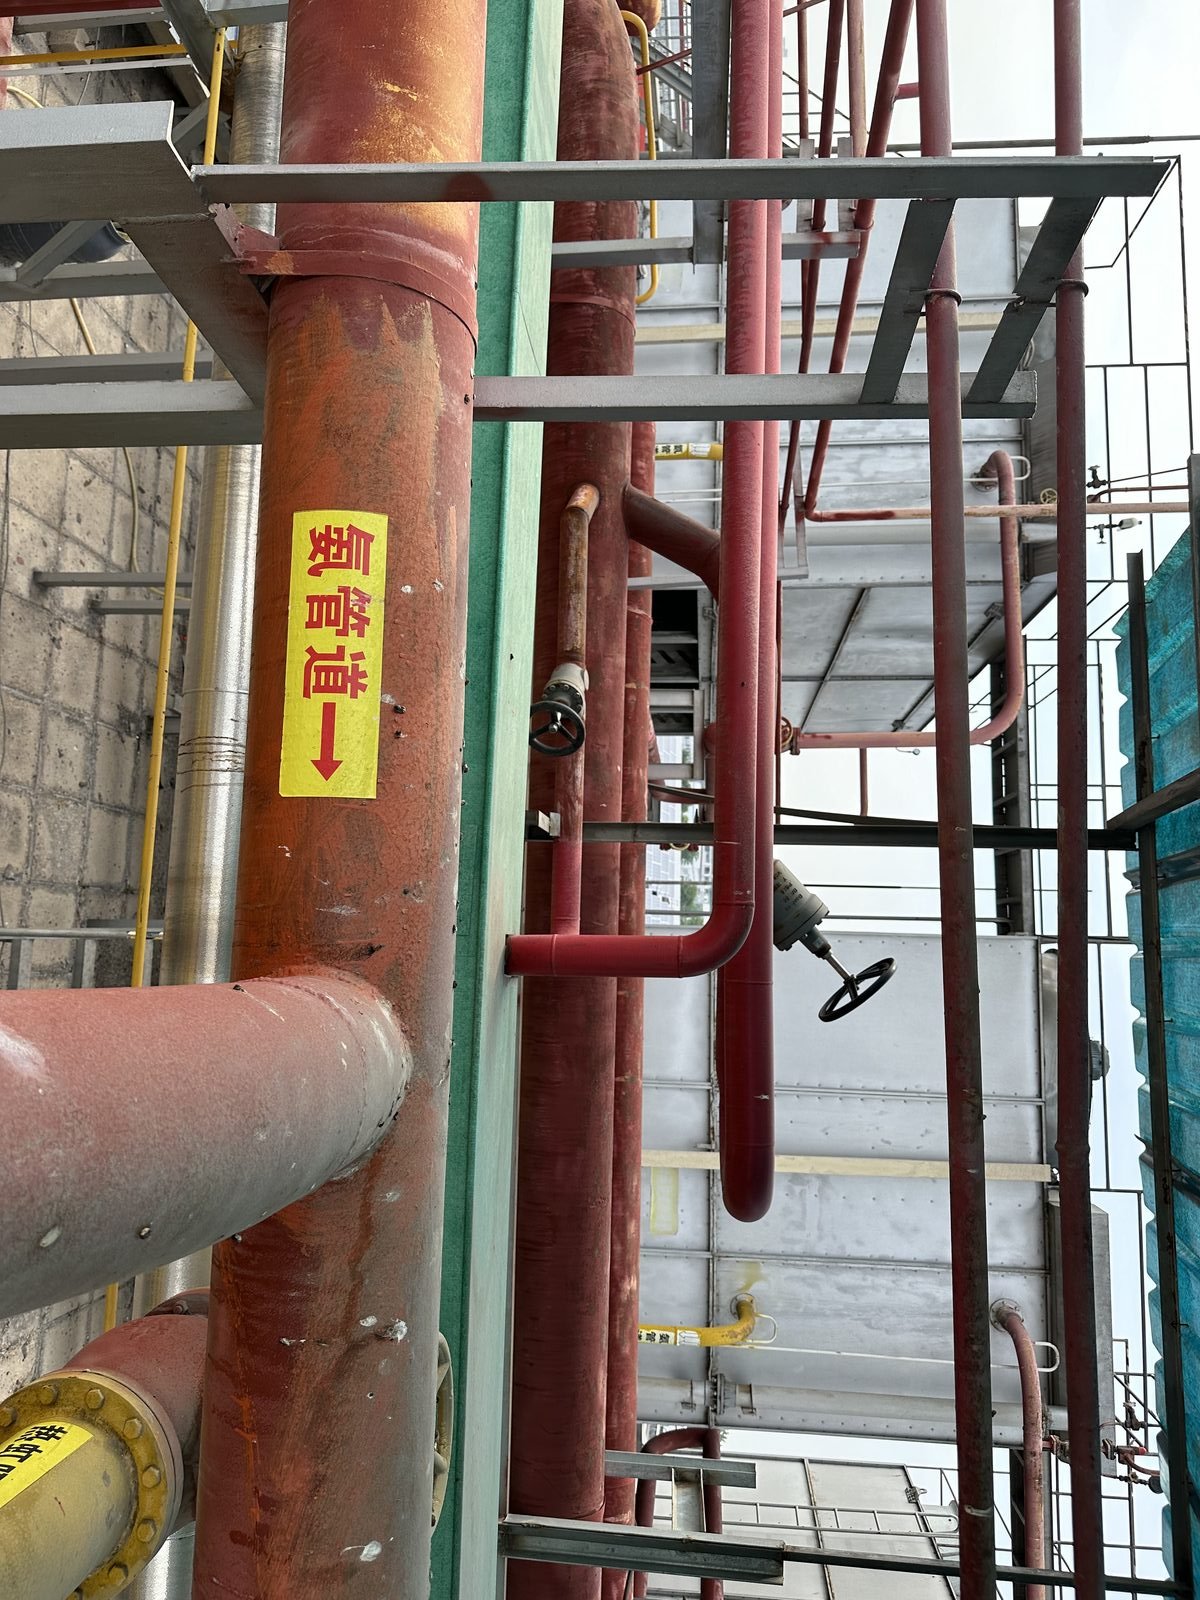
Author field survey (2024-05): ammonia mid-temp heat pump coupled to the plant refrigeration train via preheater + condenser-evaporator; plant-reported ~400–500 m³/day hot water displacing purchased steam.
Engineering data
- Case type
- Anonymized field reference — engineering experience without publishable raw data
- Data status
- Anonymized field reference
- Data source
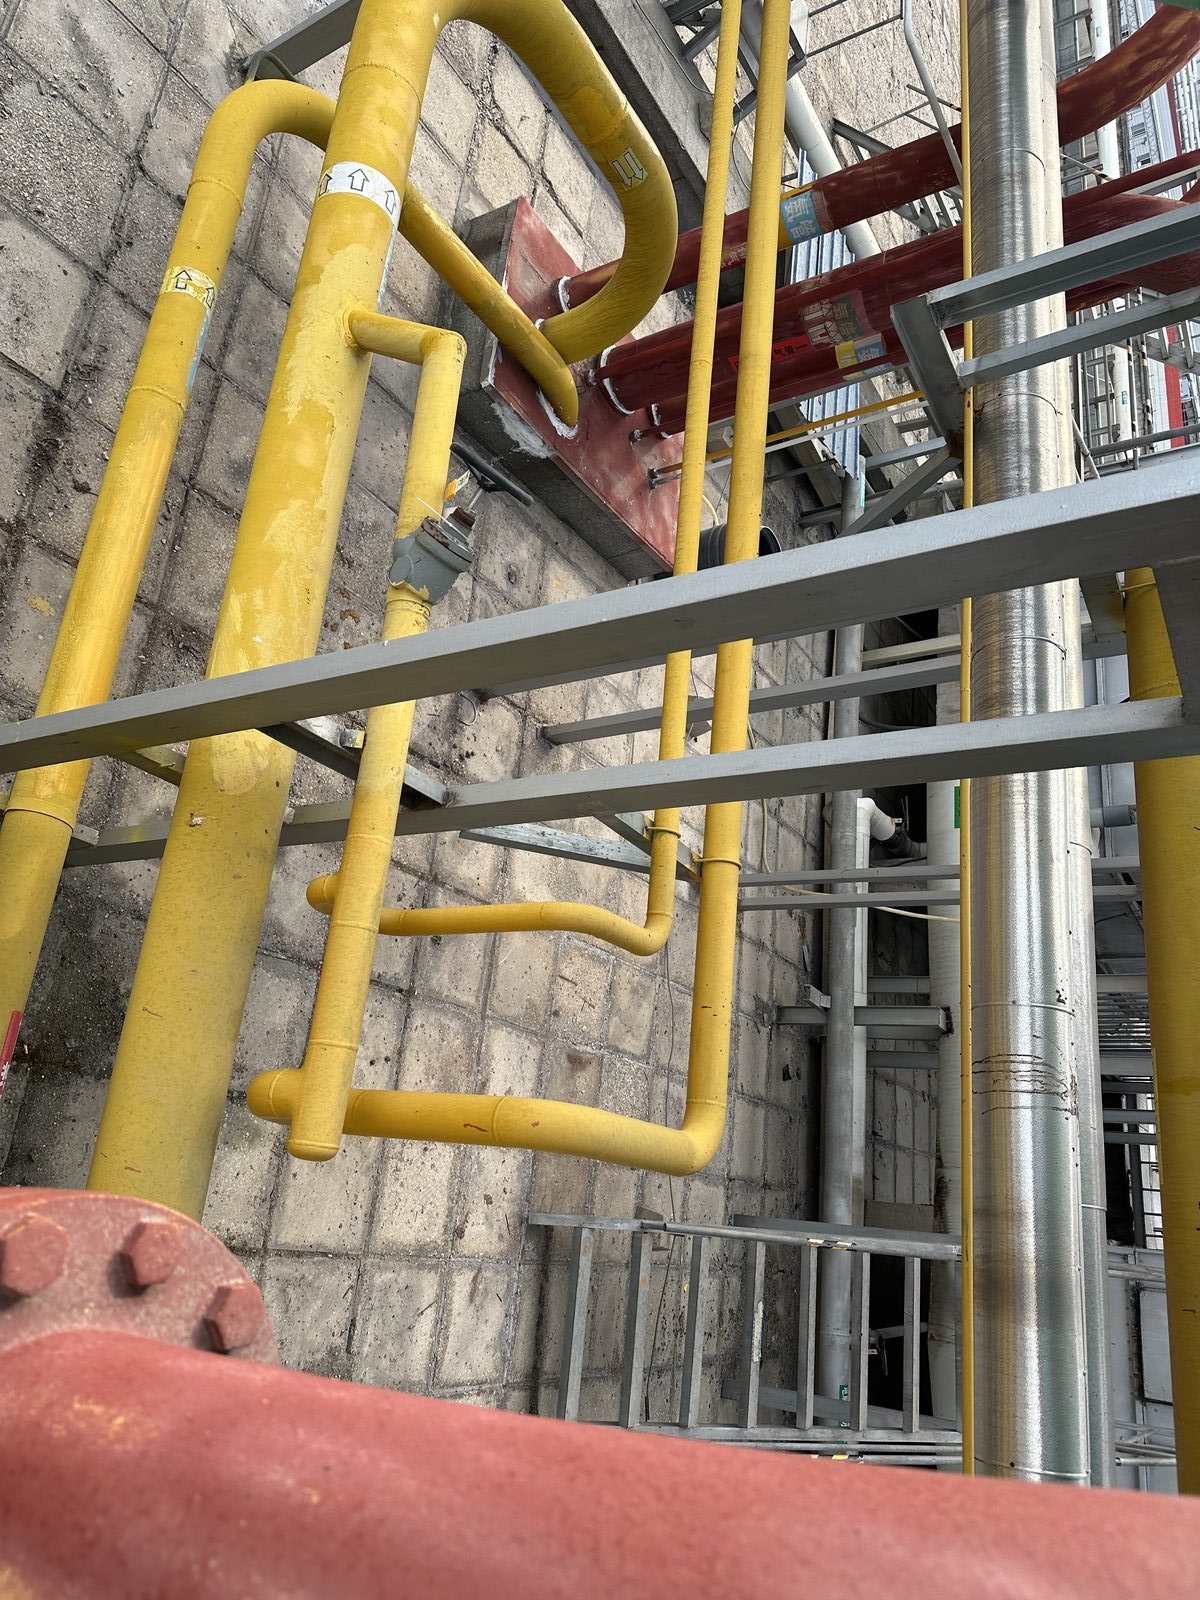
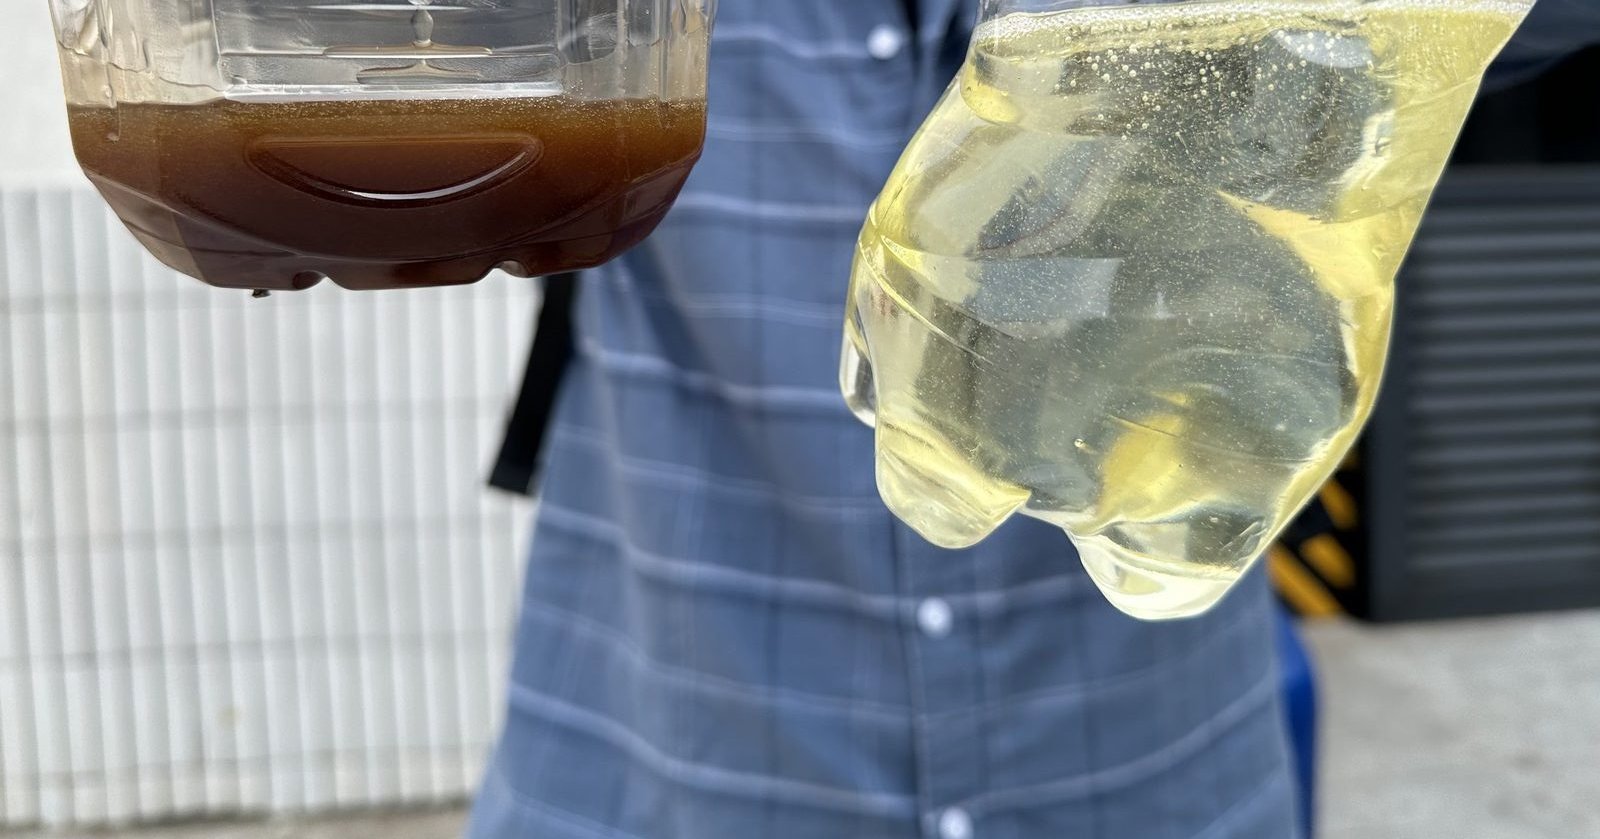
- Author site survey notes (2024-05); plant-reported hot-water volume and steam-cost savings; anonymized field photographs of ammonia HP piping and package
- Reviewer / date
- Editorial (Open Thermal AI) · 2026-11-02
- Industry
- Food
- Source temperature
- 28–35°C
- Sink temperature
- 55–75°C
- Temperature lift
- ≈ 20 K
- Heating or cooling duty
- Not disclosed
- Architecture
- Ammonia mid-temperature heat pump coupled to live refrigeration via preheater + condenser-evaporator + auxiliary receiver liquid path
- Result status
- May 2024 survey record: Overall operation reported as good; steam purchase displaced for a large share of plant hot-water duty
- Key risk
- First-year oil change mandatory for the surveyed lubricant grade; piping cleanliness; prefer skid-packaged preheater + condenser-evaporator for future builds
- Existing system
- Purchased steam for process / sanitation hot water; ammonia refrigeration reject heat available on the discharge / condenser side
- Refrigerant
- R717 (ammonia)
- COP
- Not disclosed
- Annual energy / emissions savings
- Plant-reported: ~¥130k/month (~¥1.56 M/year) steam-cost savings vs purchased steam — not independently metered here
- Estimated payback
- Plant-reported: CAPEX ~¥2.6 M/set; static payback under ~1.8 years — site-specific tariffs
Project background
A Central China meat-processing plant needed large volumes of process hot water while rejecting ammonia refrigeration heat. The author surveyed the ammonia heat-pump retrofit in May 2024. Customer identity is omitted.
Narrative inputs
Source: ammonia discharge / condenser heat via preheater + condenser-evaporator. Sink: plant hot water, plant-reported ~400–500 m³/day. Heating capacity and COP not published as independently metered values on this site.
Heat pump solution
An ammonia mid-temp heat pump evaporates against refrigeration reject heat and delivers heat to the plant hot-water loop. Liquid from the preheater and condenser-evaporator returns via the auxiliary receiver path. Field notes also flag packaging the two exchangers as one skid and simplifying the inlet header for future designs.
COP & savings
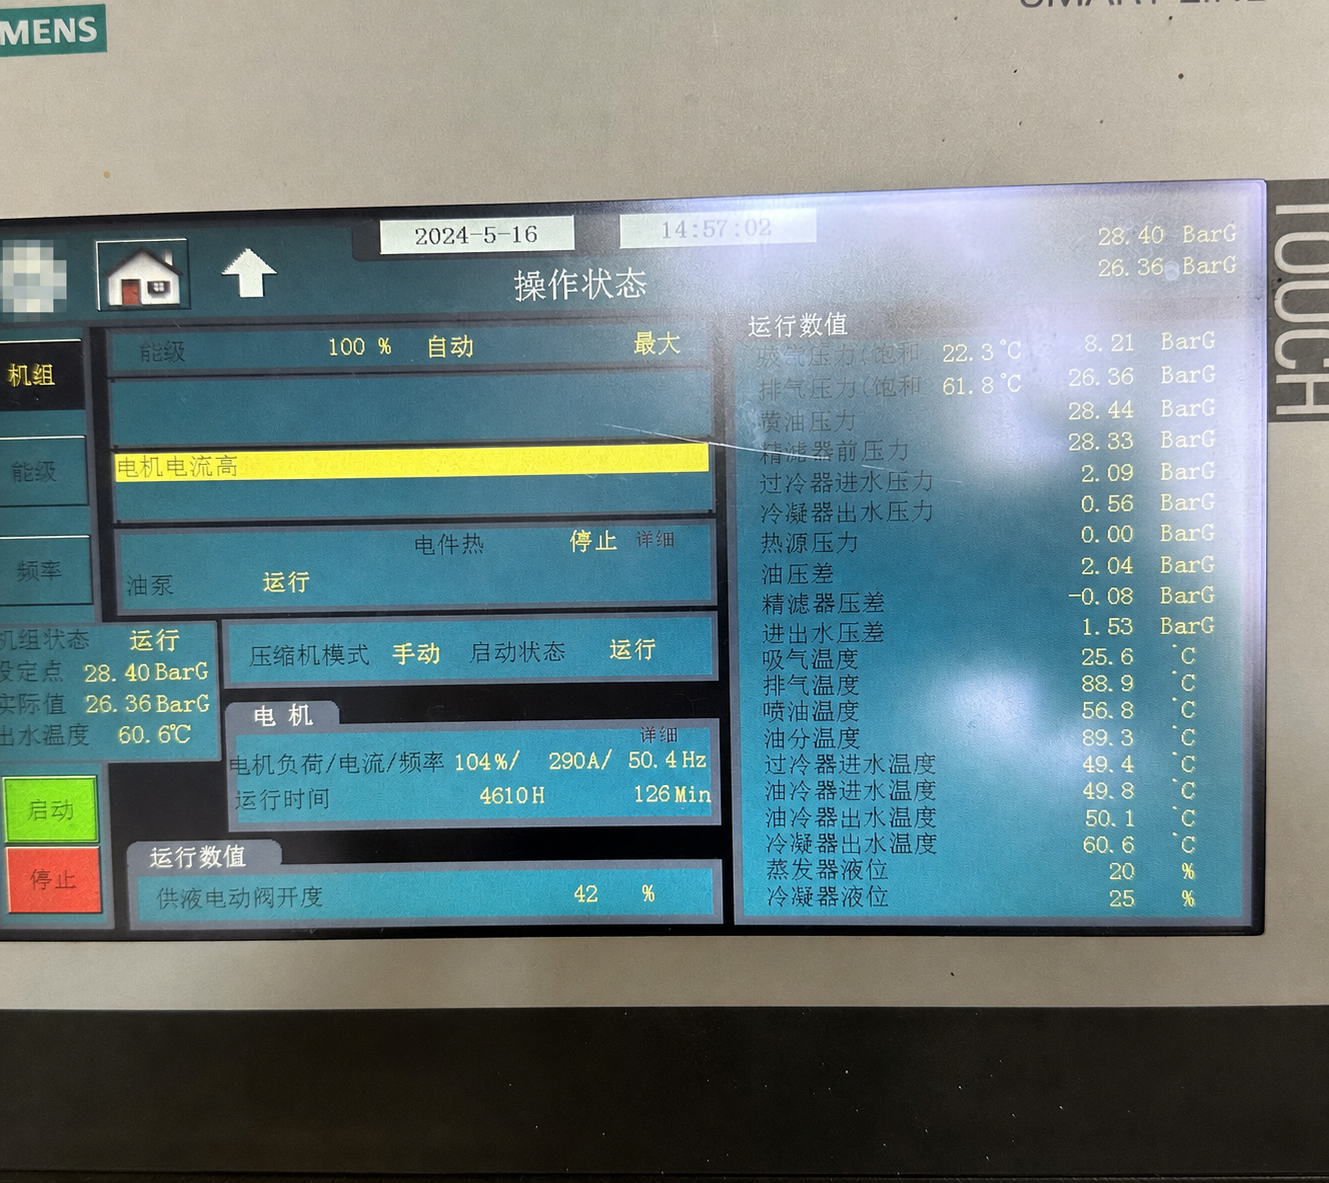
Field survey by the author; economics and daily hot-water volume as reported by the plant — not independently metered on this site. HMI snapshots from the visit show the package in normal running status; they are observational evidence only.
Investment / ROI notes
Plant-reported figures: ~¥130k/month steam savings (~¥1.56 M/year) against CAPEX ~¥2.6 M/set, implying static payback under ~1.8 years. Tariffs, hours, and steam price are site-specific; treat as site-reported, not verified ROI.
FAQ
Is this a verified measured project?
No. Evidence level is anonymized field reference: author site survey notes and photographs plus plant-reported economics. Independent metering was not performed for this publication.
How does this differ from other food ammonia HP cases on the site?
This case centers on Central China meat-plant hot water displacing purchased steam, with documented preheater / condenser-evaporator / auxiliary-receiver coupling and first-year oil / cleanliness lessons from a 2024 field survey—not a published parameter-table summary of a different region.
What should another plant verify before using this case?
Verify refrigeration operating conditions, hot-water temperatures and flow, simultaneous demand, electricity and displaced-heat costs, auxiliary power, backup heat and maintenance. Retain the safety review of the live ammonia system. This anonymized field reference does not establish your plant’s COP, net savings or payback; those require site-specific measurements and engineering review.
What changed in the 2 November 2026 review?
This was an editorial review, not a repeat site visit. No new author field record was supplied. The May 2024 observations and plant-reported savings remain historical, anonymized references; current operation and savings need a new authorized follow-up.